Featured Core Substrates for Hybrid Cabinetry
Engineered foundation panels engineered to bond seamlessly with stone-coated textures, metal veneers, and architectural composites.
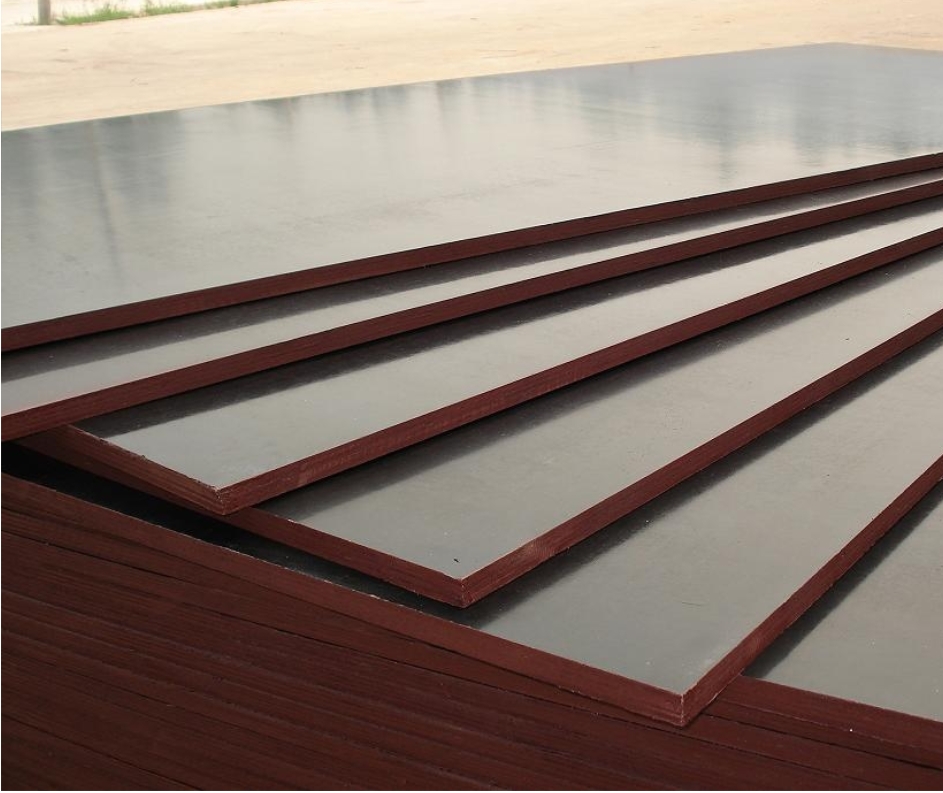
Heavy-duty phenolic barrier core providing structural rigidity for industrial cabinet framework.
Structural Base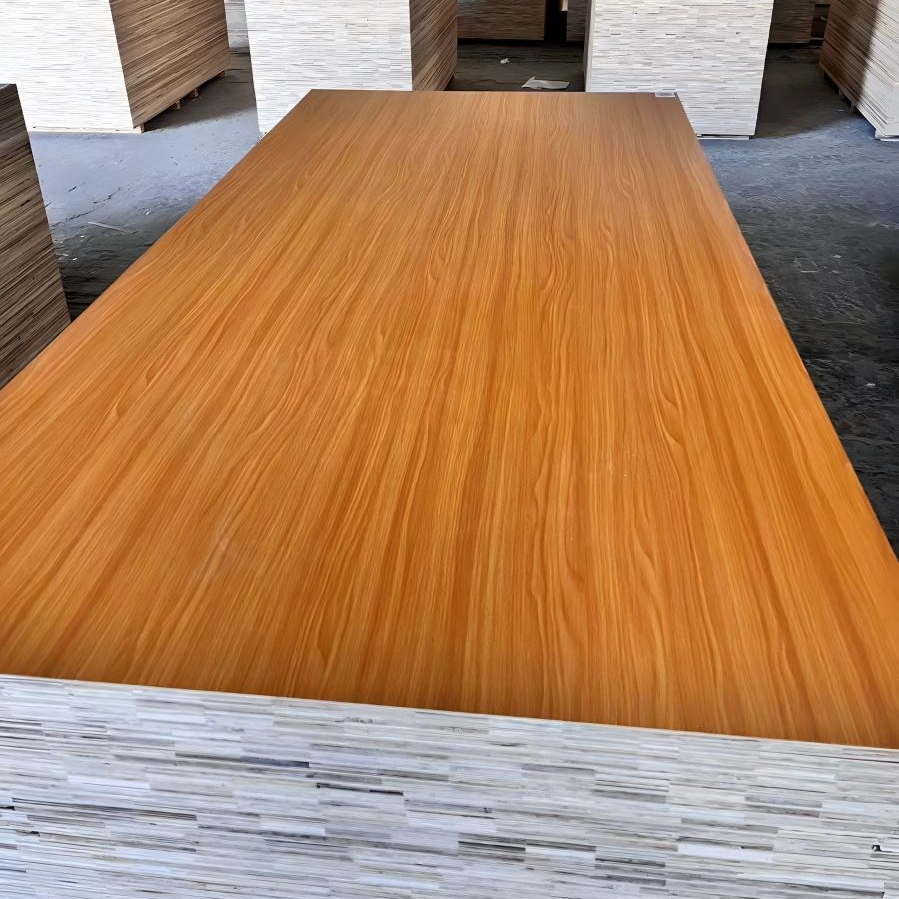
Dimensional stability optimized for interior cabinet carcass systems and textured facing.
Cabinet Grade
100% waterproof polymer composite used in wet-room and exterior outdoor cabinetry.
Waterproof Core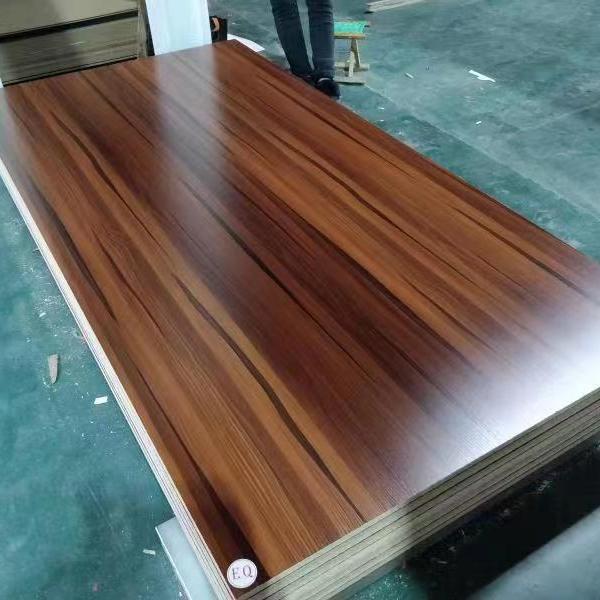
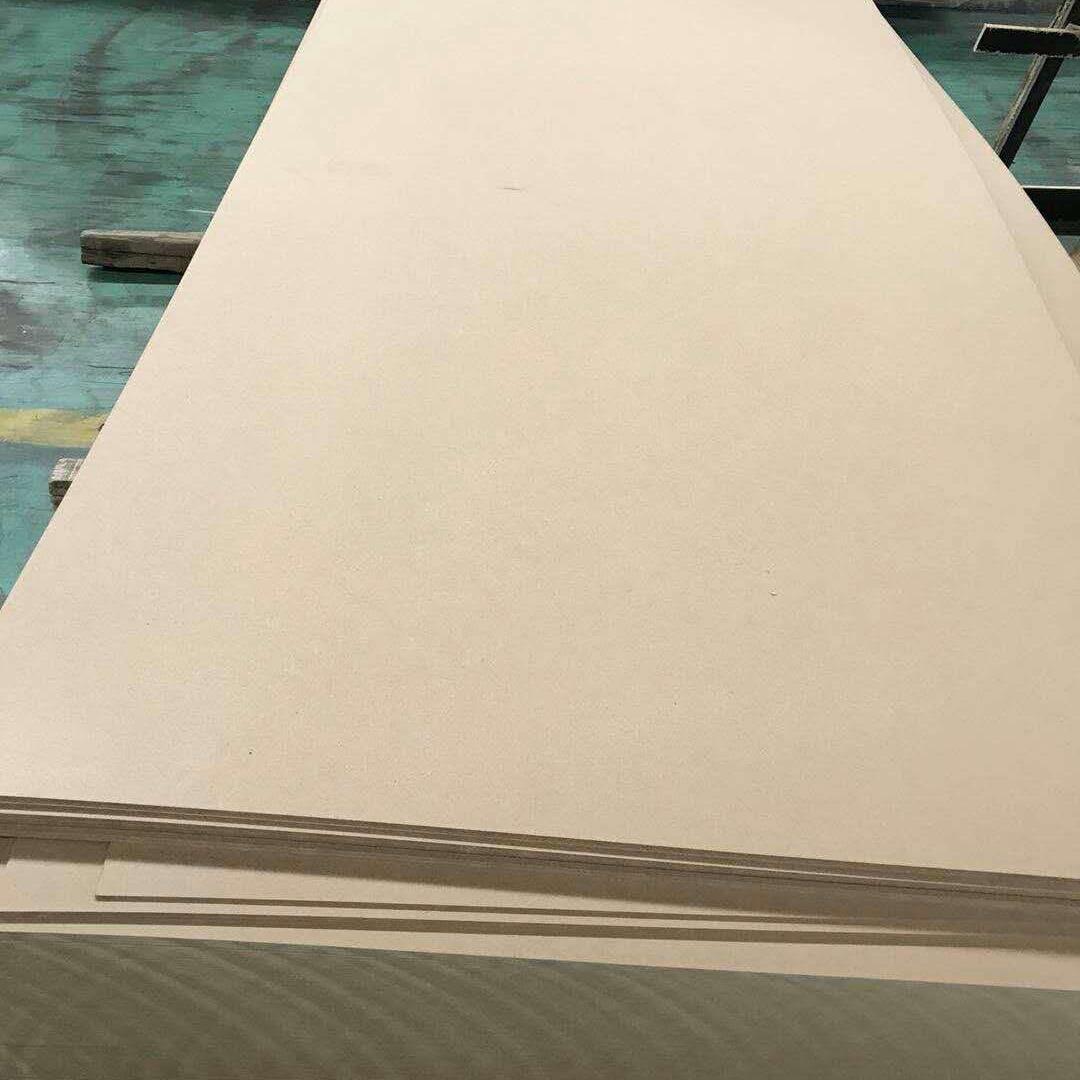
Ultra-smooth substrate ideal for precision CNC cutting and stone-coated skin lamination.
Precision BoardIndustrial Evolution: Stone Coated Material Technology in Modern Cabinet Production
Bridging heavy-duty architectural durability with precision interior & exterior joinery engineering.
Extreme Environmental Resilience
In the current commercial landscape, traditional kitchen and storage cabinetry faces severe performance constraints when exposed to UV radiation, coastal humidity, thermal shock, and chemical abrasives. The adaptation of stone-coated metal roofing technology—combining alu-zinc steel backing with ceramic-coated volcanic granule matrixes—has emerged as a game-changing exterior envelope for modular cabinetry. By fusing high-density engineered wood boards with stone-metal hybrid surfaces, cabinet fabricators can deliver fireproof (Class A), rot-proof, and impact-impervious installations designed for exterior hospitality, luxury outdoor kitchens, and heavy-duty industrial casework.
Structural Substrate Synergy
A critical engineering hurdle in metallic stone tile cabinetry is thermal expansion and acoustic dampening. High-performance cabinet manufacturing utilizes cross-laminated structural plywood, high-moisture-resistant (HMR) melamine chipboards, and hollow polymer formwork panels as damping cores. When combined with polyurethane reactive (PUR) hot-melt adhesives, these engineered wood cores eliminate hollow resonance, stabilize dimensional tolerances under extreme temperature fluctuations (-40°C to +80°C), and ensure seamless joinery for hinges, drawer slides, and cam-lock fittings.
Market Trajectory & Global ESG Trends
According to recent building materials market analytics, the global demand for hybrid architectural composite panels is projected to grow at a CAGR of over 7.8% through 2032. Commercial architects and bespoke millwork contractors are demanding cradle-to-cradle recyclable materials that eliminate volatile organic compounds (VOCs). The synergy between sustainable engineered wood cores compliant with ISO 14001 certifications and inert natural stone granules meets the highest Green Building and LEED environmental prerequisites worldwide.
Advanced Application Scenarios: Where Stone Coating Meets Cabinetry
From residential outdoor luxury to high-security industrial housing, explore how this hybrid manufacturing methodology performs.
1. High-End Outdoor Kitchens & Coastal Hospitality Casework
Standard timber cabinetry degrades rapidly when exposed to salt spray, rain, and intense UV rays. By integrating stone-coated tile technology over HMR particle boards and waterproof film faced plywood bases, outdoor kitchen carcasses achieve unmatched weatherproof longevity. The natural basalt stone granule texture mimics solid granite or quartzite slabs while weighing 70% less, dramatically reducing structural load on rooftop terraces and luxury marine vessels.
2. Heavy-Duty Industrial Enclosures & Electrical Control Consoles
In demanding industrial workshops, chemical facilities, and manufacturing plants, tool cabinets and electronic server enclosures require high impact resistance, electrostatic safety, and non-flammable casing. Utilizing stone-coated metallic laminates mounted on fireproof MDF and structural LVL timber beams provides electromagnetic shielding, thermal insulation, and scratch resistance that outlasts conventional powder-coated sheet metal.
3. Prefabricated Modular Housing & Mobile Architectural Pods
Modern modular construction relies heavily on offsite prefabrication. Integrated casework—such as built-in wardrobe partitions, exterior utility lockers, and structural kitchen modules—benefits immensely from composite panels that serve dual purposes: interior aesthetic cabinetry and exterior-grade weather barriers. This dual functionality streamlines construction cycles, lowers transport weight, and guarantees seismic resilience.
4. Commercial Retail Displays & High-Traffic Public Joinery
Public airport kiosks, bank service counters, and luxury retail fixtures face relentless mechanical wear. Stone-coated tactile surfaces offer sophisticated architectural aesthetics with high scratch-proof durability. Coupled with precision CNC-machined melamine-faced panels, retail designers can create sweeping curves, complex geometric silhouettes, and integrated LED channels without sacrificing structural rigidity.
Material Performance Matrix: Hybrid Stone-Coated Substrates vs. Conventional Cabinet Boards
| Performance Attribute | Conventional Wood Cabinetry (MDF/PB) | Full Stainless Steel Cabinetry | Stone-Coated Composite Engineered Cabinetry |
|---|---|---|---|
| Weather & UV Resistance | Poor (Swelling / Surface Fading) | Moderate (Prone to Water Spots / Glare) | Excellent (Inert Ceramic Granules / Zero Fade) |
| Fire Safety Rating | Class B / Class C | Class A (Heat Conductive) | Class A Fireproof Barrier & Thermal Dampening |
| Impact & Scratch Proofing | Moderate (Vulnerable to Gouges) | Low (Easily Scratched & Dented) | Superior (Crushed Basalt Matrix Dissipates Force) |
| Weight to Strength Ratio | Standard (~650-750 kg/m³) | Very Heavy (~7850 kg/m³) | Optimized (~550-680 kg/m³ with core routing) |
| Acoustic & Resonance Damping | Moderate | Poor (Loud Metallic Ringing) | Acoustically Deadened by Plywood/MDF Core |
About Linyi Aisen Wood Products Co., Ltd.
Over three decades of manufacturing excellence, global export logistics, and uncompromising quality assurance.

Global Industry Leadership
Linyi Aisen Wood Products Co., Ltd., officially renamed as Aisen Wood in 2019, is a premier manufacturing titan in the wood and composite building materials sector based in Linyi, Shandong Province, China. With over three decades of unbroken operational expertise, we operate as a fully vertically integrated enterprise covering scientific R&D, structural design, automated precision pressing, global distribution, and dedicated after-sales engineering support.
Our technical mastery spans the full spectrum of structural sheet goods, film faced concrete formwork, premium furniture-grade melamine boards, high-moisture-resistant particle boards, and innovative composite substrates engineered for cutting-edge cabinet and architectural cladding production.
Strict Quality Control & Testing Systems
Maintaining unyielding quality is the cornerstone of our manufacturing philosophy: "Survival by quality, development by reputation." Our in-house testing laboratory conducts rigorous, batch-by-batch evaluations on core performance parameters including static bending strength, modulus of elasticity (MOE), formaldehyde emission rates, moisture equilibrium, and boiling water immersion peeling tests.
Our extensive sales network serves key commercial markets across South America, North America, the Middle East, Africa, Southeast Asia, and Australia, earning the enduring trust of cabinet makers, modular builders, and civil engineering conglomerates.

01. QUALITY GUARANTEE
Good products start from good raw materials. We employ more than 45 dedicated quality inspectors overseeing every phase from veneer peeling to hot pressing and final calibration.
Learn More →02. OUR SERVICE
Pre-sales Service: Any inquiry will be replied within 24 hours. After-sales Service: Any quality issues will be analyzed and resolved within 24 hours by technical specialists.
Learn More →03. CERTIFICATE
Our commitment to manufacturing excellence and environmental safety is recognized through our ISO 9001 quality system certification and ISO 14001 environmental certification.
Learn More →
Full Engineered Product Portfolio for Cabinet & Construction Systems
Browse our certified range of film faced panels, furniture-grade melamine boards, and structural substrates.
Cost-effective phenolic coated multi-ply board for structural cabinet reinforcement.
Heavy-Duty Core
Attractive wood-grain aesthetic combined with high screw-holding power.
Cabinet Grade
Ultra-lightweight polymer hollow core panel, 100% moisture and insect proof.
Eco Polymer
Ultra-flat calibrated density fiberboard for precision CNC profiling & skin adhesion.
Precision Substrate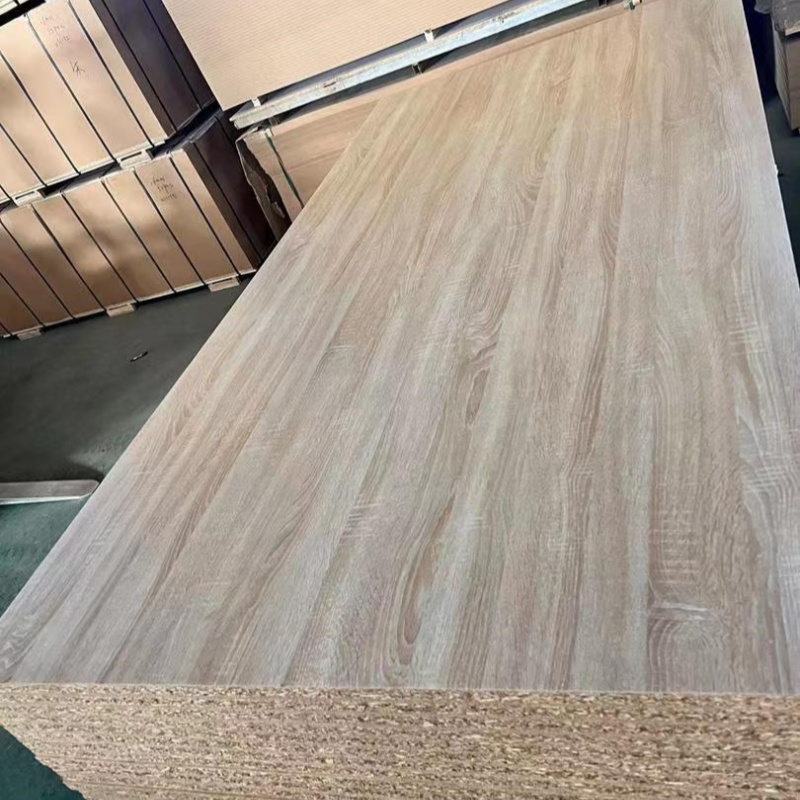
High Moisture Resistant particle board tailored for bathroom and kitchen carcass boxes.
HMR Standard
Heavy structural LVL framework beams engineered for massive architectural casework.
Structural LVL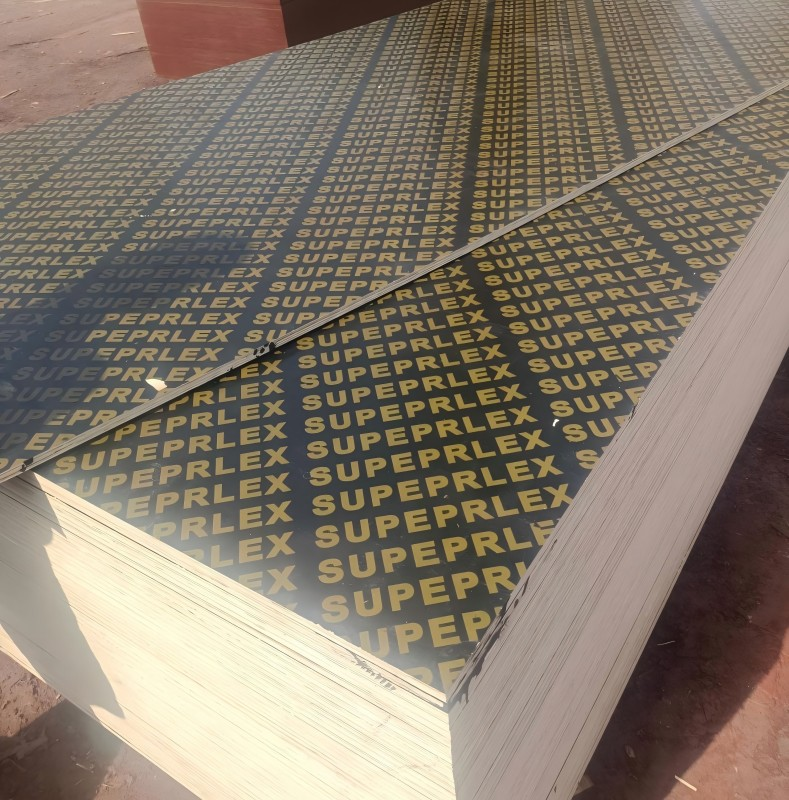
Economical building sheet stock for temporary cabinetry, backing plates, and mockups.
Economy Grade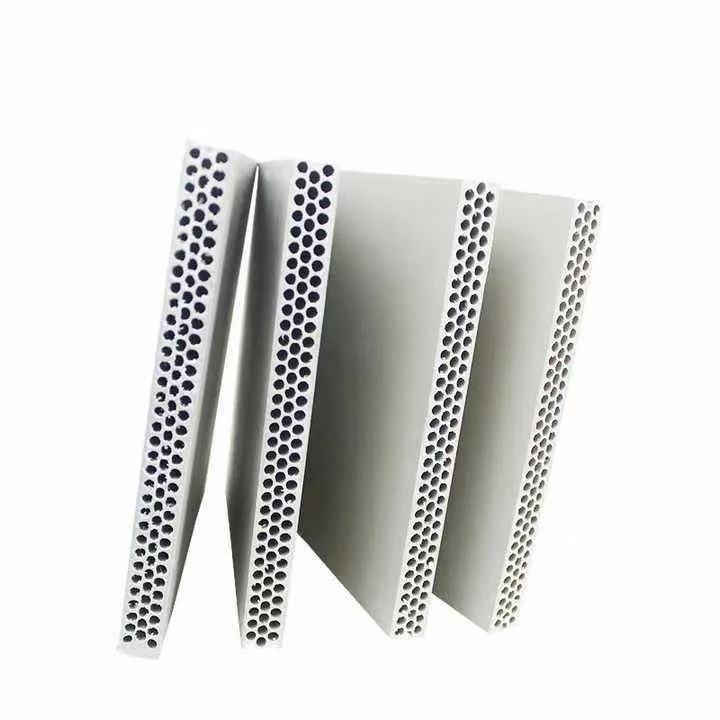
Durable recyclable composite panels designed for zero-rot exterior cabinetry.
Composite PanelSpecialized Architectural Casework & Formwork Portfolio
Full catalog range of engineered panels available for worldwide export and custom manufacturing.




-

Phone
-

E-mail
-

Whatsapp
-
Whatsapp
Judy

-
Whatsapp
Judy
-

Top